
Pet food packaging and supply chain
How a global pet food company improved its supply chain management with remote warehousing for its packaging


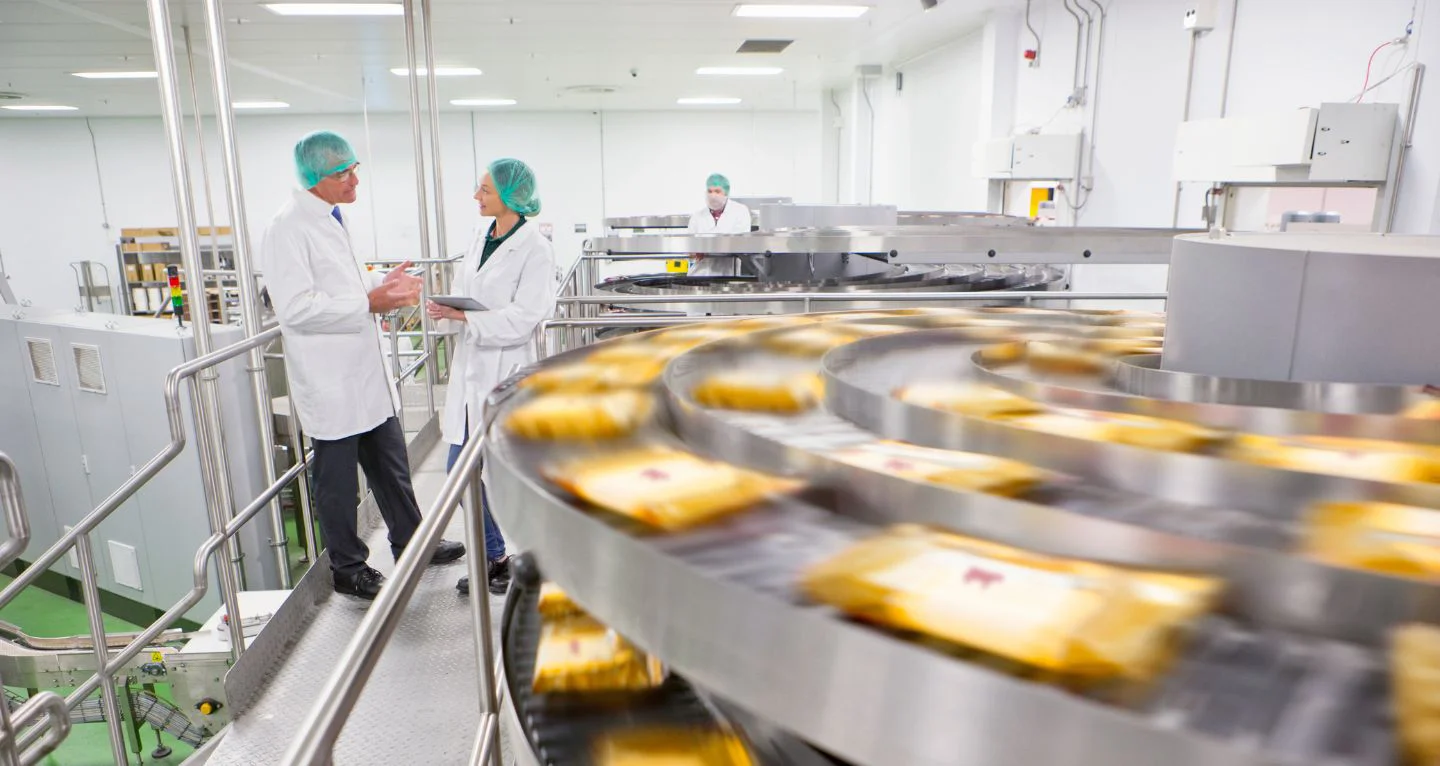
This case study highlights how a fresh cheese manufacturer improved shelf life, productivity, and film-to-machine compatibility through Velvet’s integrated solutions.
The project included both the optimization of their food packaging system and the introduction of a vertical packaging machine for grated cheese.
01
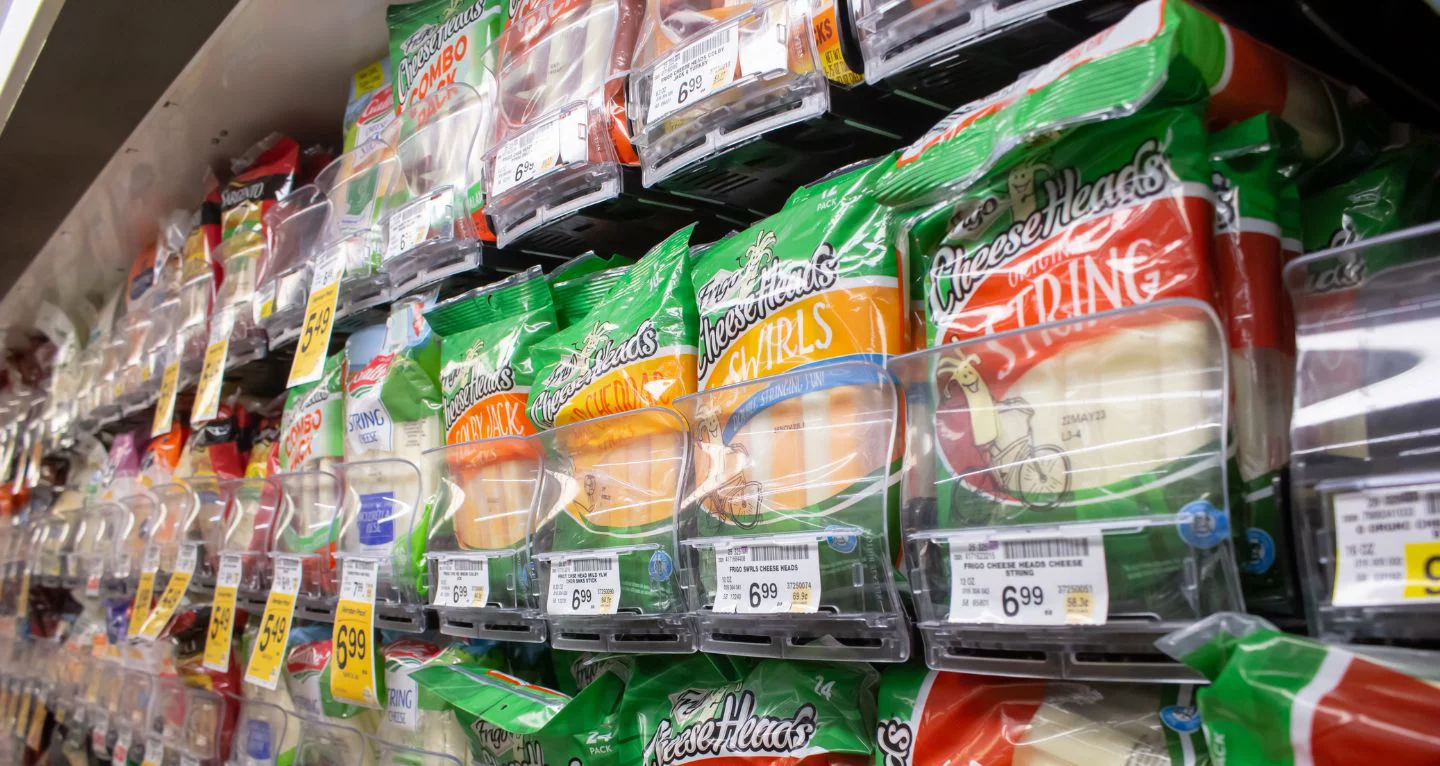
The client is a cheese producer with headquarters in San Diego, California, and a production plant in Tijuana, Mexico. The company specializes in fresh cheese formats such as sticks, mozzarella for pizza, cheese strings, and grated cheese.
With annual revenues of $50 million, it primarily serves the food service market and has recently expanded into retail, offering products under both its own brand and private label. The company’s distribution covers Mexico, Central America, and the United States.
02
The client approached Velvet with a clear need: to resolve serious packaging issues that were compromising both product quality and production efficiency.
Two major problems were identified:
03
Velvet collaborated directly with the Laferpack technical team to analyze the problem and identify the most suitable packaging film. The proposed structure was a custom barrier film specifically developed for this type of application—perfect for dairy packaging and fully compatible with horizontal flow wrapping lines.
Phase 1: Supply of transparent film for testing
Phase 2: Transition to custom-printed film after six months of successful production
Result: improved machinability, no further mold issues, and a significant increase in shelf life.
Want to learn more about our high-barrier films for food packaging? Contact us here
04
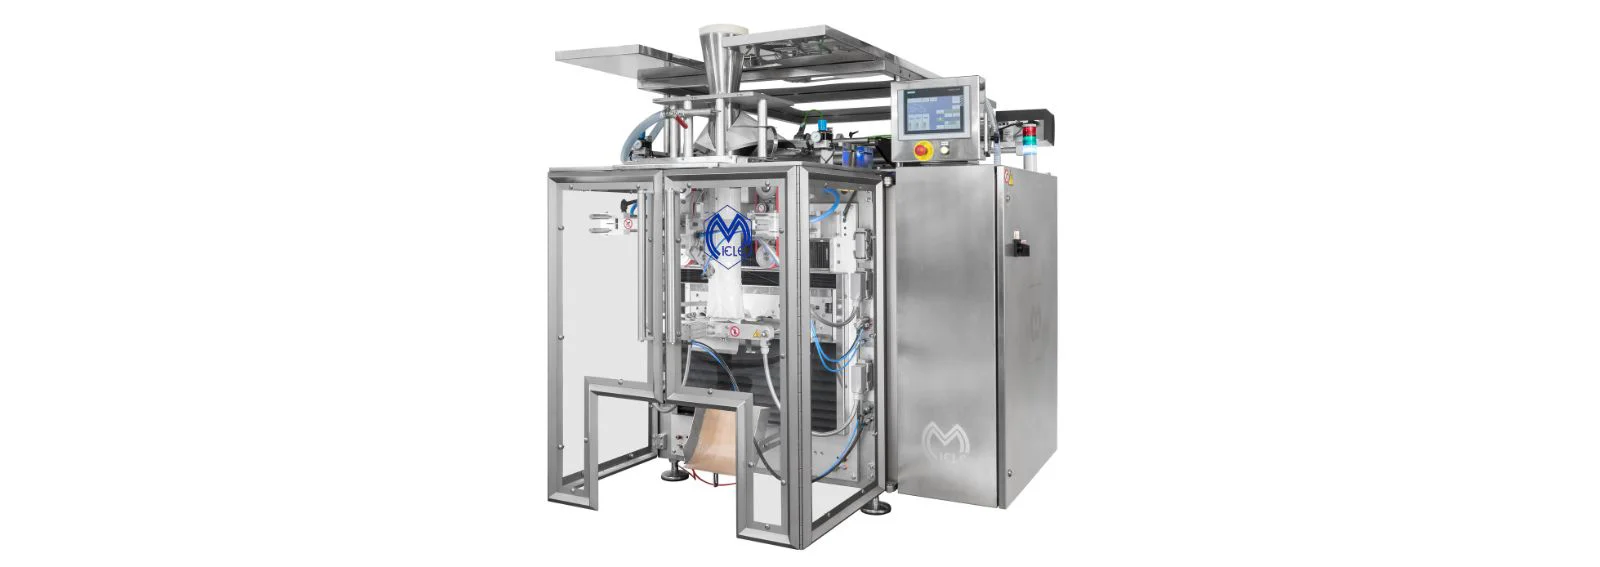
Impressed by the results achieved with packaging materials, the client also chose Velvet to supply a new vertical form-fill-seal machine, after experiencing poor post-sales support from their previous OEM.
Chosen model: Miele Maxima 400 Continuous Motion Multihead with 14 heads
Technical solution: optimization of the sealing system to eliminate film wrinkling
Curious about this machine? Explore our vertical packaging systems here.
05
06
Through a tailored, technically-driven collaboration, Velvet became a strategic partner for this Mexican dairy producer, delivering custom food packaging solutions and automated equipment that solved real production challenges. This case stands as a clear example of how material and machinery integration can drive efficiency and reliability in fresh cheese packaging.
How a global pet food company improved its supply chain management with remote warehousing for its packaging